
Fully Automatic Light Steel Keel Packaging Equipment Innovative Light Steel Keel Packaging Machine
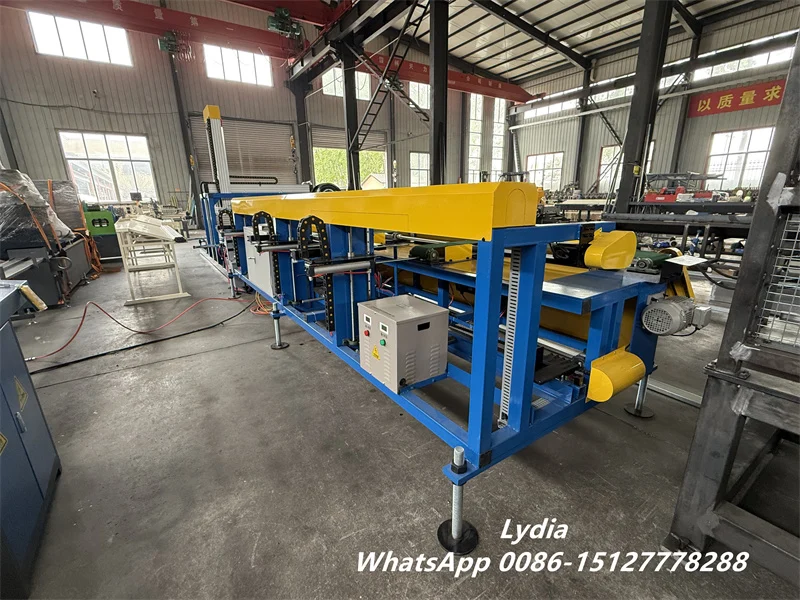
Fully Automatic Light Steel Keel Packaging Equipment Innovative Light Steel Keel Packaging Machine
The light steel keel strapping machine developed and manufactured by our company is a new product developed to meet market demand. It has applied for multiple patents, greatly improving production efficiency, reducing labor intensity, improving product qu
Detailed Content
1、 Overview
The light steel keel strapping machine developed and manufactured by our company is a new product developed to meet market demand. It has applied for multiple patents, greatly improving production efficiency, reducing labor intensity, improving product quality, and reducing safety accidents.
2、 Main components and working principle
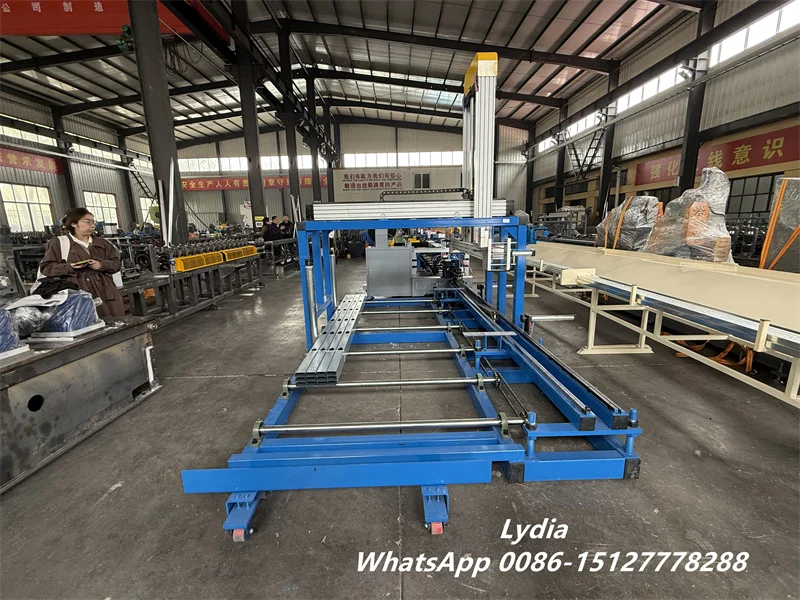
The equipment mainly consists of a packaging machine (including conveying, fastening, stacking, tidying, winding, material positioning, etc.) and a palletizing machine (including 2-axis palletizing, conveying, and telescopic roller conveyor).
Working principle: This device is used to achieve the interlocking, stacking, winding tape, palletizing, and removal of light steel keel for forklift. Easy to operate, intelligent parameter setting, completely replacing manual labor.
3、 Main parameters
1. Input power supply voltage: three-phase five wire AC 380V ± 10%, 50Hz (or customized).
2. Input power capacity: 8KW (AC).
3. Input gas source pressure: 0.6Mpa~0.8Mpa. An air storage tank should be equipped on site, and a single device should be equipped with an air compressor with a displacement of 0.5 cubic meters or more per minute.
4. Inlet height: 750~800mm (or customized).
5. Packaging and wrapping material: tape/strapping (default tape, or customized).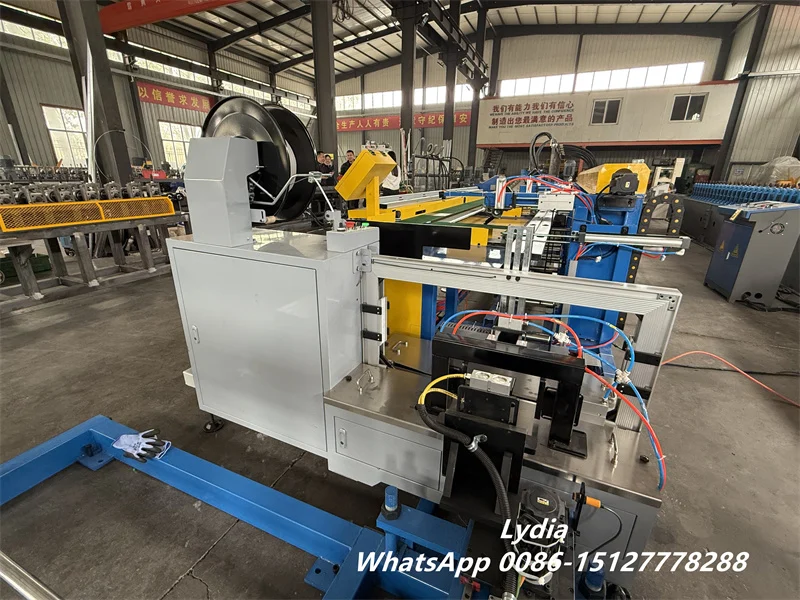
4、 Operation Guide
1. Connect the gas source to check for air leaks, connect the power supply and wait for the touch screen to enter the system
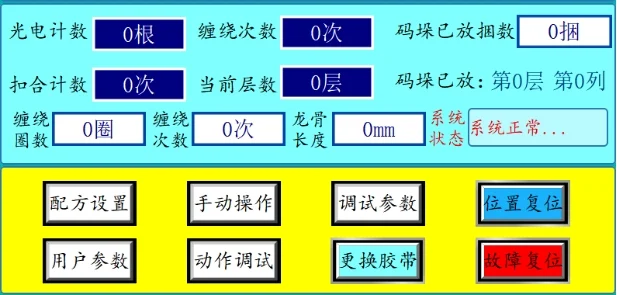
2. Observe whether the displayed values on the monitoring screen (blue and the display box for the number of bundles already placed in the stack) are consistent with the actual values. If they are not consistent, first modify the quantity on the screen to be consistent before proceeding to the next step
After completing the parameter settings, confirm that the current position is the initial or normal position, and then turn the [Manual/Auto] knob on the operation panel to automatic to start production.
If it is not in the initial position, you can open the "Manual Debugging" interface and manually adjust it to the initial position, or when rotating to automatic, a prompt box will pop up on the page. Follow the prompt to reset to the initial position
If there is a malfunction, press the emergency stop button or simultaneously press the emergency stop button and the host to stop. The emergency stop button will include a host stop function, which will stop together with the host after the emergency stop.
After troubleshooting, release the emergency stop and observe the system status. If there are no other faults, it will display that the host has not been reset. Press and hold to start the machine.
Common parameter modification
The monitoring screen displays numerical values such as {photoelectric count} {deduction total} {winding times} {current number of layers} {number of bundles already placed in the stack}. Click the input box to pop up the numeric keyboard, and enter on the keyboard (modify according to the actual value on site)
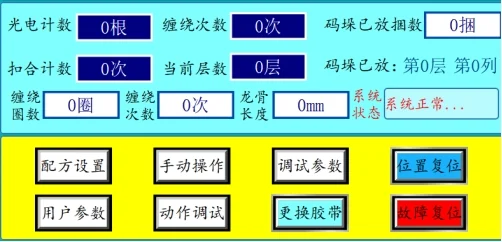
Number of winding turns: number of tape winding turns during packaging
Winding times: The number of times the keel is wrapped during packaging, automatically dividing the size evenly
Dragon bone length: When packaging, the length of the dragon bone is set according to the actual length
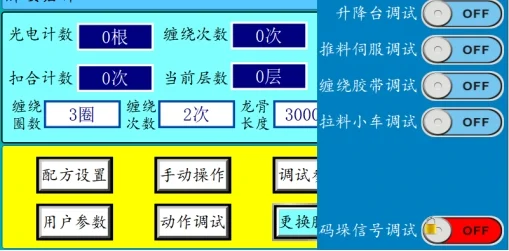
3. Action debugging
Different opening methods can be selected according to the stop position of the keel (if the keel needs to be wound and stopped, it can be switched to automatic mode, and the winding tape debugging can be started directly from the winding)
4. User parameters: time parameters and speed parameters, which can be adjusted according to actual conditions
Tape position adjustment: The tape position can be adjusted according to the actual situation, and the error can be automatically calculated by correcting the tape position
IO monitoring: Real time monitoring of PLC input and output status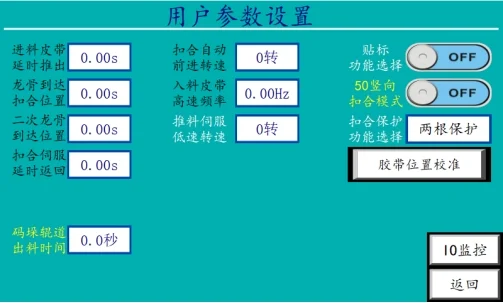
5.
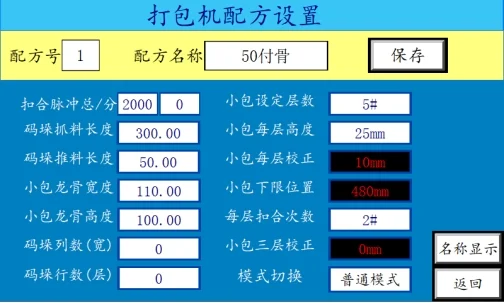
Total number of fastening pulses: the degree of flipping of the toggle during fastening
2) Number of pulse buckles: degree of flipping of the first paddle
3) Stacking pushing length: pushing distance during stacking (cannot be set too long, otherwise it may cause stacking axis alarm or damage)
4) Width of small package keel: width of small package keel after winding
5) Height of small package keel: height of small package keel after winding
6) Number of stacking columns (width): How many rows of small package keels are stacked in total
7) Stacking rows (height): How many layers of small package keel are stacked in total
8) Number of layers for small package setting: Number of layers for small package before wrapping
9) Height of each layer of the small package: height of each layer after the keel is fastened
10) Correction for each layer of the small package: offset height of the lifting platform
11) Lower limit position of small package: lower limit position of lifting platform
12) Number of buckles per layer: How many rows of keels per layer for small bags
13) Small package 3-layer correction: Correction of the falling position of the 3-layer during the 2-layer winding mode of the small package
14) Mode switching: divided into normal mode/vertical mode/two-layer winding mode
Formula setting method: First, modify the formula number, find a blank formula, modify the corresponding parameters, and set the name. click Press and hold the button for 1 second until it disappears. Complete recipe saving.
Recipe calling method: Find the previously saved recipe number, enter it into the recipe number input box, and check if the name is the recipe you want to call.
ClickPress and hold the button for 1 second until it disappears. Complete the recipe call.
Debugging parameters: including basic parameters for device operation, including time parameters, speed parameters, mechanical parameters, device parameters, I/O definition parameters, etc. The parameters involve the operation of the equipment, please coordinate with the manufacturer for modification.
Name Display: Can display the name of the currently stored data
Manual operation debugging interface
Manual operation: Click the button according to the text to complete the operation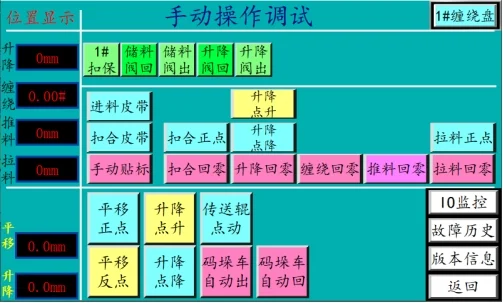
When pulling the material back to zero, check if the position is consistent with the actual situation. If it is inconsistent, reset it to zero first and then return to zero.
Pay attention to checking for any objects when returning to zero
Daily maintenance of equipment
Clean up the garbage in various parts, such as the feeding belt driving the keel and the zinc slag falling off the keel.
Check if there is a lack of lubricating oil in the oil-water separator. If there is a lack, add lubricating oil, model turbine 1 oil ISOVG32.
Is there too much water accumulation in the oil-water separator? If there is too much water accumulation, manual drainage is required.
Regularly inspect the drainage of the gas storage tank, check daily in summer and every 3 days in winter.
Each sliding component such as slider, nut, bearing component, etc. needs to be lubricated weekly, and components such as gearbox need to be lubricated monthly.
Common fault handling
What should be done after changing the specifications of the keel
After changing the specifications of the keel, the first step is to modify the formula page according to pages 6 and 7. Secondly, the position of the equipment fastening protection cylinder and the lifting platform baffle needs to be adjusted according to the width of the keel.
How can I adjust the number of times I want to wrap the dragon bone tape
On the left side of the monitoring screen, in the packaging area, set the number of winding circles input box according to page 4
What parameters need to be adjusted for different lengths of dragon bones
On the left side of the monitoring screen, adjust the length of the keel in the packaging area
Parameter input error, collision, status display. How to handle a certain servo fault
Firstly, turn off the manual/automatic knob, press and hold the fault reset button, and see if the displayed servo fault can be removed. If the fault cannot be reset, manual power-off and restart are required. After restarting, see if the fault can be reset. If the fault can be reset, manually adjust the servo position and remove the keel. Then reply to the location and reopen.
How to deal with the cold bending machine not turning
Check if the emergency stop is released and if the screen displays a fault.
After troubleshooting, the cold bending machine usually does not run because the screen shows that the host has not been reset. Press and hold the fault reset button again. This fault is to ensure that the operator confirms that the problem has been resolved before turning on the cold bending machine to prevent danger.